
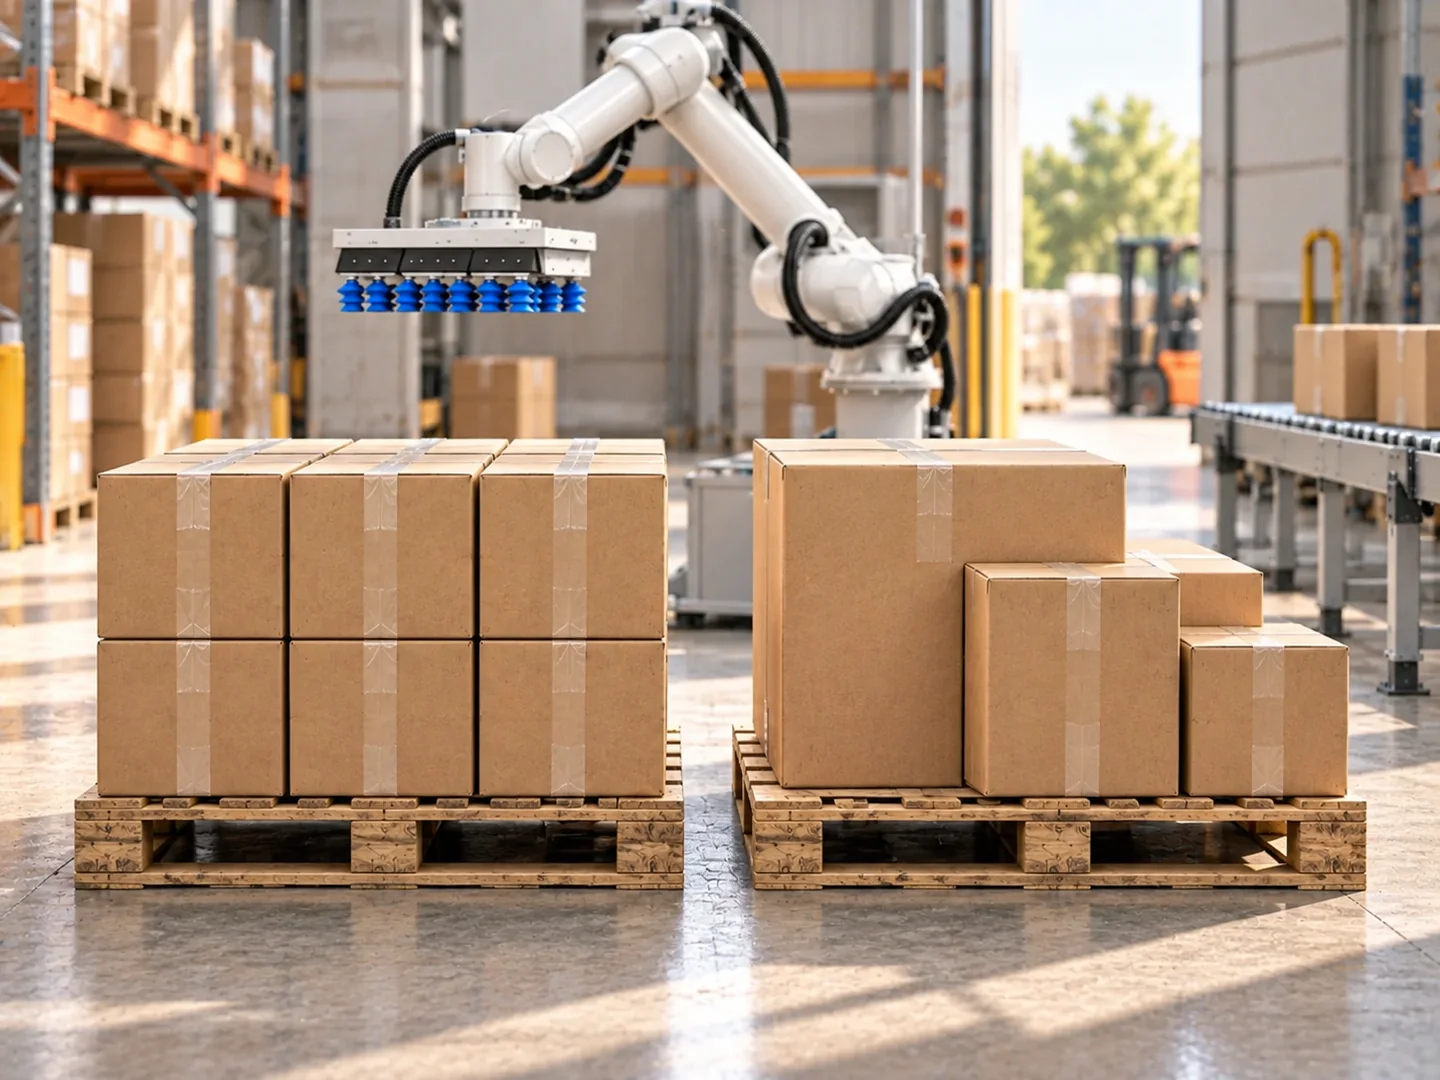
Mixed-case palletizing builds a pallet from different products or carton formats. Single-SKU palletizing repeatedly stacks one product type. SKU means stock-keeping unit: the identifier a business uses for a particular product variant.
The distinction changes more than the robot programme. Different carton sizes, weights and arrival sequences can change gripping, buffering, stacking rules and the information required before each placement.
Separate three receiving jobs
Collecting cartons on a pallet, building a repeated single-product pattern and constructing a mixed order pallet are different requirements. Specify which one the client actually needs.
Prime Robotics’ mixed-case explanation describes the category as combining products with different sizes, weights and identifiers on one pallet. Dedicated systems address identification and load planning as well as robot movement.
A container unloading robot that transfers cartons onto a pallet has not necessarily produced a load with an approved shipping pattern, product sequence or stability assessment. Confirm those responsibilities separately.
Use this overview to define which job you need, then keep the detailed decisions with their owners: software and move confirmation, arrival order and buffers, and finished-load support and stability. A supplier proposal should identify the boundary between extraction, physical handoff and accepted pallet building. The two receiving layouts illustrate where those responsibilities can separate; they are not validated cell designs.
Compare the inputs each job needs
| Design question | Single-SKU load | Mixed-case load |
|---|---|---|
| Carton data | One product’s filled dimensions and mass | Data for every allowed product and relevant variation |
| Arrival order | Often a repeated, known carton stream | May need identification, routing and sequence control |
| Grip and placement | Repeated contact and release geometry | Different carton surfaces, sizes and clearances |
| Pattern planning | A defined repeated load pattern | A plan accounting for the actual mix and load rules |
| Buffering | Handles interruptions and pallet exchange | May also hold cartons until the required sequence is available |
| Acceptance | Validate the expected repeated product | Validate representative product combinations and exceptions |
These are specification questions, not guaranteed characteristics of every machine. Even a nominally identical product can arrive in cartons with changed board quality, tape, deformation or contents distribution.
Work through two sample workflows
Illustrative single-SKU workflow: cartons of one known product arrive on a prepared conveyor. The line establishes a repeatable pick position, and a robot places cartons according to an agreed pattern. Pallet exchange and damaged cartons remain explicit parts of the operation.
Illustrative mixed-case workflow: a receiving line sees several product types. The system identifies a carton, checks its dimensions or stored product data and decides whether it can be placed next. A carton that does not fit the current sequence may need a buffer, another destination or operator review.
Both workflows are examples, not KRONA operating modes. Their difference is useful when deciding what equipment and software belong downstream of unloading.
Choose the finished-pallet job before selecting the robot
A useful request names the output: cartons collected temporarily for receiving, a repeated single-SKU pallet, or an order-specific mixed pallet released for transport. The same product mix can lead to a different equipment brief when the finished load has a different destination.
For a carton-palletizing application, supply the expected carton source and an example of the accepted finished load. Keep the first assessment bounded to a declared carton set and pattern. Add mixed arrivals or changing order rules as explicit requirements rather than assuming they follow from a successful repeated placement.
KRONA AGV or forklift transport can move the completed pallet within the agreed application, but that movement does not validate its pattern or stability. Agree who releases the pallet for collection and what happens to a partial load that is not yet ready.
Define the load rules before promising output
Ask the client for maximum pallet height and mass, allowed overhang, carton orientation, compression limits, wrapping requirements and destination restrictions. Identify whether the pallet must support put-away, transport or a store-specific unloading order.
Do not assume that filling unused space produces an acceptable pallet. A compact arrangement still needs the application’s load and handling requirements verified. Use representative completed loads to evaluate the result.
If a supplier uses a pallet planning algorithm, ask what data it needs, what it does when that data is missing and how a changed carton is detected. “Mixed-SKU capable” needs an agreed operating envelope.
Match arrival order to pallet-building order
Inside a floor-loaded container, extraction can be constrained by which carton faces are accessible. That sequence may differ from the order needed for a planned mixed pallet.
Map the steps between the two: identification, inspection, routing, temporary storage and release to the cell. Decide how unknown products and damaged cartons leave the sequence. Use the palletizing cell design guide to turn those decisions into a layout.
A larger buffer can cover a short interruption or hold a small sequence mismatch. It cannot indefinitely absorb more cartons than the downstream operation completes. Quantify the rates with the line-capacity worksheet.
Trace an arrival sequence before sizing the reorder buffer
Consider an illustrative sequence exercise, with an already approved placement order A → B → A → C. The letters identify carton types, not a validated pallet pattern. Arrivals are B → A → C → A, and the planning rule releases any available carton matching the next required type before processing the next arrival.
| Arrival | Decision under the example rule | Completed order | Cartons waiting after the decision |
|---|---|---|---|
| B | Hold B; the next required type is A | None | B |
| A | Place A, then release the waiting B | A → B | None |
| C | Hold C; the next required type is A | A → B | C |
| A | Place A, then release the waiting C | A → B → A → C | None |
The trace has a maximum of one waiting carton after processing each arrival. If the arrivals change to B → C → A → A, the same rule needs two waiting positions before the first A arrives. Arrival order has changed the illustrative reorder requirement even though the four-carton mix is identical.
These counts assume instantaneous decisions and completion before the next arrival. They are not physical buffer specifications: carton dimensions, travel, identification, placement time and new arrivals during a cycle can require additional capacity. Test the actual arrival and service timing with the capacity guide.
The unloading robot’s accessible extraction order also need not match the pallet order. Identification, routing and sequence control belong to the downstream design unless the project explicitly assigns them elsewhere; KRONA’s pallet handoff alone does not establish mixed-case pattern planning.
Download the arrival-sequence log to record a real arrival time, carton identity, intended next placement, routing decision, waiting count and outcome. Retain the log before and after any proposed sequencing change. This worksheet is blank; the example above is not measured customer evidence.
What to send when assessing unloading
For a detailed project brief, use the guides for mixed SKU unloading and carton sorting, mixed-pallet support and load validation, timed sequencing and reorder buffers, and palletizing software requirements. Each addresses a separate decision between inbound extraction and the accepted finished load.
Provide representative carton data, the product mix by load, current arrival order and the intended receiving destination. Explain whether boxes are collected, sorted into single-SKU pallets or sent to a dedicated mixed-case palletizing process.
KRONA U1 handles eligible floor-loaded closed cardboard cartons up to 25 kg with conveyor or pallet handoff. Arbitrary mixed-case stacking and load optimisation are not established by those capabilities.
The conveyor-or-pallet handoff guide helps define the boundary. Request a freight and receiving assessment with the actual carton mix and downstream requirements.
- palletizing
- cardboard cartons
- warehouse automation
KRONA U1 unloads boxes from containers onto pallets or conveyors and also loads containers with boxes from pallets or conveyors. Explore KRONA U1 →
Assess your carton palletizing application