
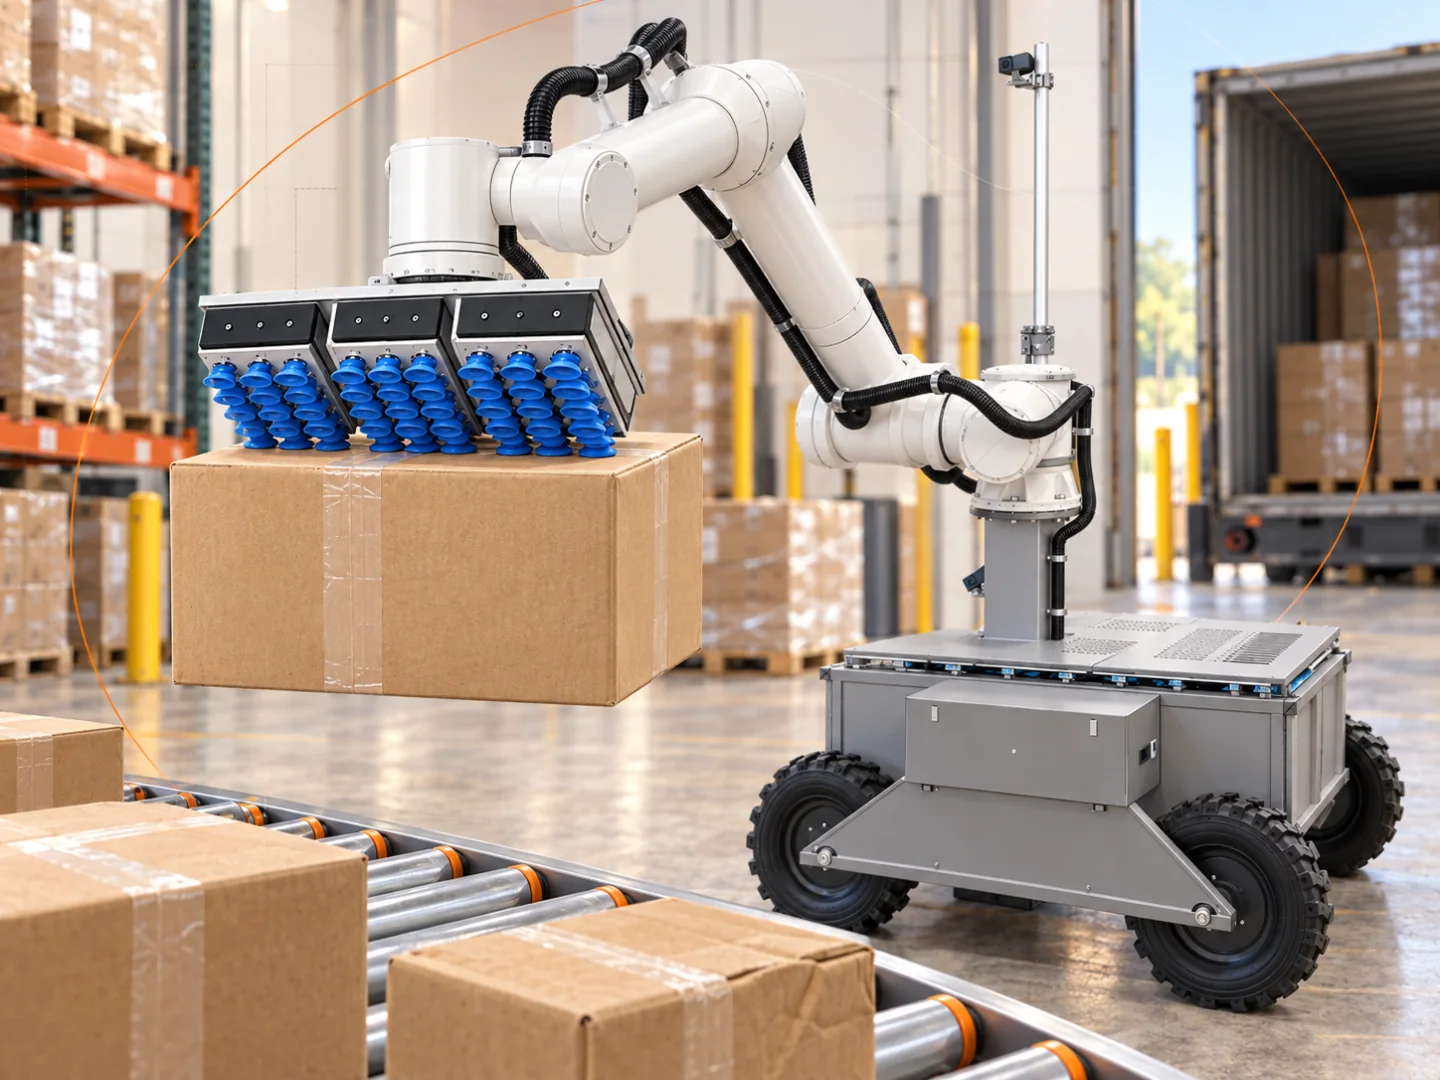
A vacuum gripper can lose a carton because the seal never formed, air leakage weakened the hold, the carton wall deformed or the movement imposed a load the grip could not retain. The stage where the failure occurs is often more useful than the single observation that “the robot dropped the box.”
Use the diagnostic worksheet below to organise observations with the responsible engineer. It is an assessment method, not a record of measured KRONA failures or a universal set of control settings.
Identify the failing stage
Separate contact, vacuum build-up, extraction, transfer and release. Record the carton and contact position, then associate the event with the stage where the behaviour changed.
A grip that fails before extraction presents different questions from one that holds during a pause but releases during acceleration. A carton that sticks at placement may have a release problem rather than insufficient holding force.
First confirm the package and tool are within the application’s approved operating conditions. Follow the equipment’s approved inspection and recovery procedure before examining hardware or the load.
Use a symptom-to-test worksheet
| Observed symptom | Candidate cause to investigate | Evidence to record |
|---|---|---|
| Vacuum does not build at contact | Contact gap, uncovered area, leak or supply problem | Contact-face image and vacuum trace |
| Hold weakens during a pause | Leakage through board, seal or circuit | Vacuum over time and carton condition |
| Panel dents while the tool remains attached | Local panel strength or unsupported contents | Deformation before and after the pick |
| Grip holds statically but fails in travel | Motion load, orientation or contact-point effect | Failure stage, approved trajectory and load details |
| Tape or a label detaches with the tool | Adhesion to the board weaker than the applied load | Surface attachment and the actual contact patch |
| Carton does not release cleanly | Release sequence, residual vacuum or mechanical interference | Placement and withdrawal sequence |
The candidates are hypotheses. Several can produce the same symptom, so log observations before changing a configuration.
Distinguish vacuum level from leakage flow
Vacuum level describes the pressure difference. Air flowing through porous board, a contact gap or an uncovered section can prevent the system from maintaining it during the cycle.
A larger pump or a stronger commanded vacuum is not automatically the correct change. The contact geometry, leakage path, available supply and panel behaviour need to be examined together. Piab’s cardboard-handling discussion explains why leakage and package deformation matter.
For tool selection rather than diagnosis, see the carton and cardboard-box gripper guide.
Preserve the service and carton history together
Retain the relevant tool configuration, service-event reference and carton-profile version beside the symptom log. Use the complete carton-test sheet to compare the same package and movement conditions; use the maintenance planning guide for documented service responsibilities and release evidence.
Test the actual transported package
An empty new carton can differ from a filled carton that has travelled inside a compressed load. Record the package’s filled weight, contents distribution, board condition and accessible face.
Include the cartons that dominate the operation and the conditions associated with the problem. Keep damaged or otherwise unsuitable packages outside the agreed test boundary until reviewed.
If a new carton type changes the result, retain both the previous and new package records. That makes it possible to distinguish a packaging change from a tooling or supply change.
Investigate motion without losing the baseline
Theoretical suction force does not establish safe retention through every movement. Load direction, acceleration, centre of gravity, friction and the strength of the carton panel affect the application.
Keep the approved settings and trajectory with each test record. If an authorised engineer changes the configuration, start a separate set of results so a later review can identify which change affected the outcome.
Use the EOAT integration checklist to check the tool, mounting, utilities and confirmation sequence together.
Keep an event record
For each test or observed exception, record:
- carton ID, filled weight, dimensions and surface condition;
- tool/configuration identifier and accessible contact face;
- start condition and stage of the failure;
- available vacuum trace and image/video reference;
- package condition after the event;
- whether a retry was authorised and its outcome;
- active assistance minutes and time to resume;
- the next hypothesis, owner and verification step.
A spreadsheet with one row per event is enough to start. Use the same definitions for a successful pick, a retry and a drop.
Example: a changed carton surface
Consider a hypothetical application that begins to lose grip after receiving a different carton design. The first record should compare the actual contact faces, board, tape position and vacuum behaviour of the two packages. It should not assume that changing a pump setting solves the problem.
If the grip forms but the panel deforms during transfer, a leak-only diagnosis would miss the package-strength question. Log that observation and have the complete package/tool/movement combination reviewed. This example illustrates the worksheet; it is not a KRONA test result.
Distinguish a diagnostic change from a validated correction
Suppose a carton profile fails more often after a packaging change. Keep the original tool, motion and measurement method as the comparison baseline, then document one changed variable at a time. Compare equivalent filled cartons and contact faces; changing the box and robot motion together makes the cause difficult to identify.
Record attempted picks as well as failures. Hypothetical example: four failures in 200 attempts is 2%; one failure in 50 attempts is also 2%. The smaller test does not demonstrate an improvement merely because it contains fewer failed picks. Keep the carton profile and the failing stage beside the rate.
After a proposed correction, repeat the complete extraction, transfer and release sequence with representative cartons. Inspect package damage and downstream behaviour. A higher vacuum reading alone cannot prove that the carton panel or grip remains sound throughout motion.
Retain the before-and-after test records and the approved configuration. Use the pilot checklist to decide whether the evidence supports the corrected profile or requires further testing.
Connect diagnosis to freight eligibility
A repeated failure may identify a correctable application issue or a carton type outside the system’s envelope. Both outcomes are useful if they establish how the operation should handle that freight.
KRONA U1 is assessed as a complete unloading system for eligible cartons. Send representative package details for an assessment, and use the pilot checklist to agree how grip reliability, assistance, damage and recovery will be measured.
- vacuum gripper
- cardboard cartons
- robotic manipulation
KRONA U1 unloads boxes from containers onto pallets or conveyors and also loads containers with boxes from pallets or conveyors. Explore KRONA U1 →
Request a freight assessment